Temprite
928R Coalescent Oil Separator
The model 928R from Temprite is compatible with most refrigerants including hydrocarbons, ammonia (NH3) and subcritical CO₂, and is designed for 44.8 bar (650 PSI).
Cette page produit n’est pas encore disponible en français : l’original en anglais est affiché.
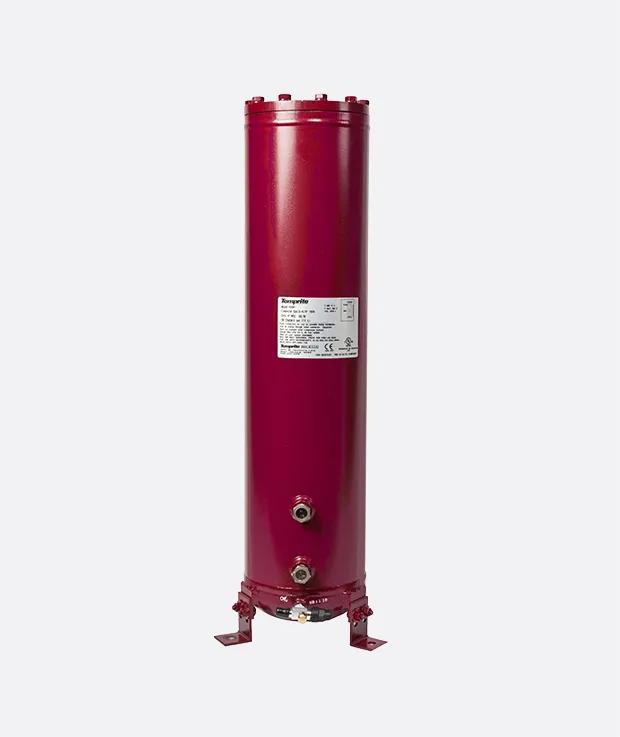
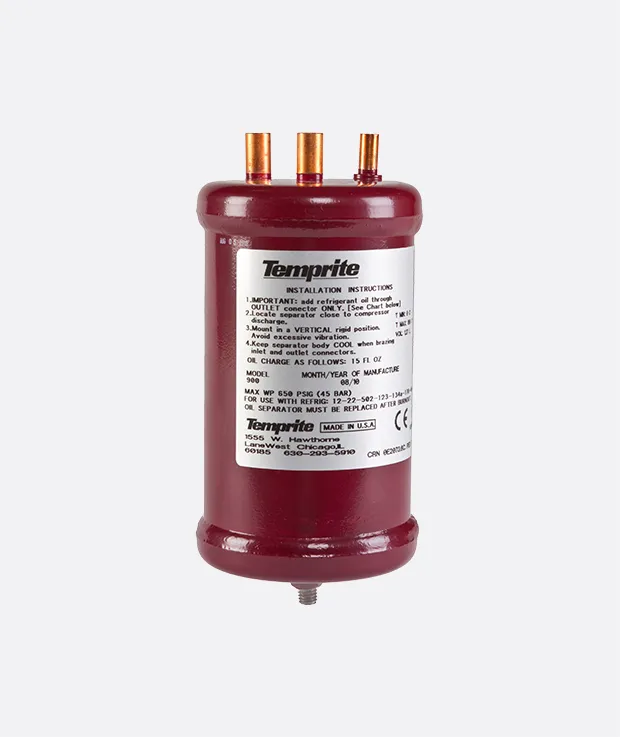
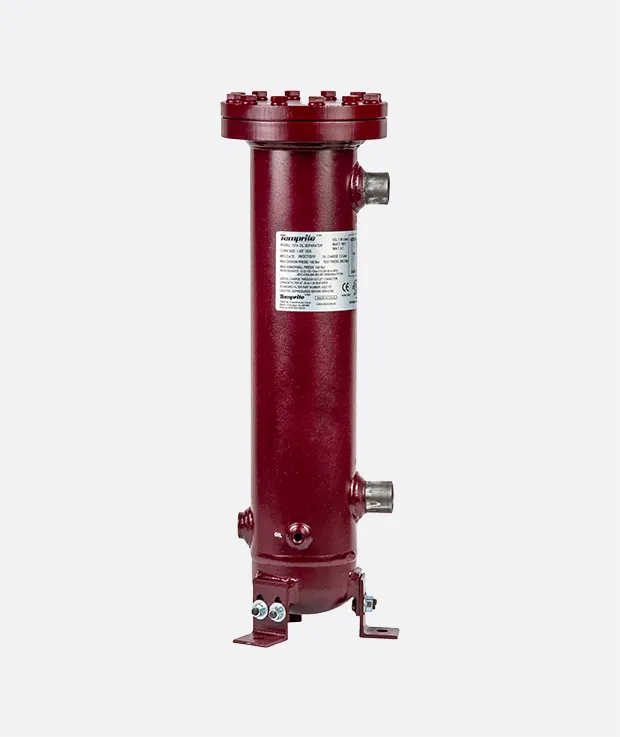
Fig. 01 — 928R Coalescent Oil Separator
01 Présentation
An oil reservoir is built into the 928R coalescent oil separator.
01
The model 928R Coalescent Oil Separator is accessible and the filter can be replaced when necessary. The “R” is for reservoir. The built-in reservoir reduces piping, components, and potential leaks and creates a stable, high pressure oil system. Because the oil reservoir is built-in, the 928R separator does not have a float. The Temprite 928R oil separator is designed to remove oil from the refrigeration system and return it to the compressor, resulting in shorter compressor run times, reduced energy consumption and the highest possible return on investment. The main purpose of the oil is to lubricate the compressor. When oil circulates instead, it builds up a film on the internal surfaces of heat exchangers and acts as an insulator. This robs the system of efficiency and raises energy consumption. Coalescing separators are capable of removing 95% to 99% of the oil component of mass flow. The glass fiber filter material is capable of exciting the smallest oil molecules. The fiber material forces the molecules to collide and form larger droplets which fall to the bottom of the separator to drain back to the compressor.
The Model 928R Coalescent Oil Separator is primarily used in larger commercial refrigeration applications that utilize traditional refrigerants. Like the rest of the 920 and 920R series, it has a replaceable filter with easy top access.
02 Dossier technique
Caractéristiques
13 données · telles que publiées par Temprite
- Fluide frigorigène
- CO₂ · R744 · Ammoniac · R717 · Hydrocarbures
- Catégorie
- Composants
01Performances
2 entrées
- Efficiency rating
- 98.5%+ nominal separation
- Filtration particulate retention rating
- .3 microns
02Limites de fonctionnement
2 entrées
- Operating pressure
- MWP: 44.8 bar (650 psi)
- Operating temperature
- Max Temp: 160 °C (320 °F)
03Fluide frigorigène
3 entrées
- Refrigerant
- R744, R717, 22-123-134a-404A-407A-407C-410A-507-410A-502-507
- Oil Charge amount
- 7.55 Liters (2 Gallons)
- Refrigerant
- Ammonia, CO₂, Hydrocarbons
04Composants et options
1 entrée
- Connection size options (npt/mm)
- ODS: 67 mm (2.625 in.)
05Construction et dimensions
3 entrées
- Height/diameters (mm/in)
- H: 940 mm (37 in.) D: 219 mm (8.625 in.)
- Volume (l/gal)
- 29.16 Liters (7.70 Gallons)
- Filter Access Clearance (mm/in.)
- 406 mm (14 in.)
06Certification et marchés
2 entrées
- Certification
- PED (CE Marked), UL and UL Canada, CRN, AU
- Region
- Africa, Asia, Australia & NZ, China, Europe, Global, Japan, North America, South America

Parlez de 928R Coalescent Oil Separator avec Temprite.
Envoyez votre demande à Temprite : demandez caractéristiques, tarifs et disponibilité pour votre projet.
Produits associés
Autres produits de Temprite →