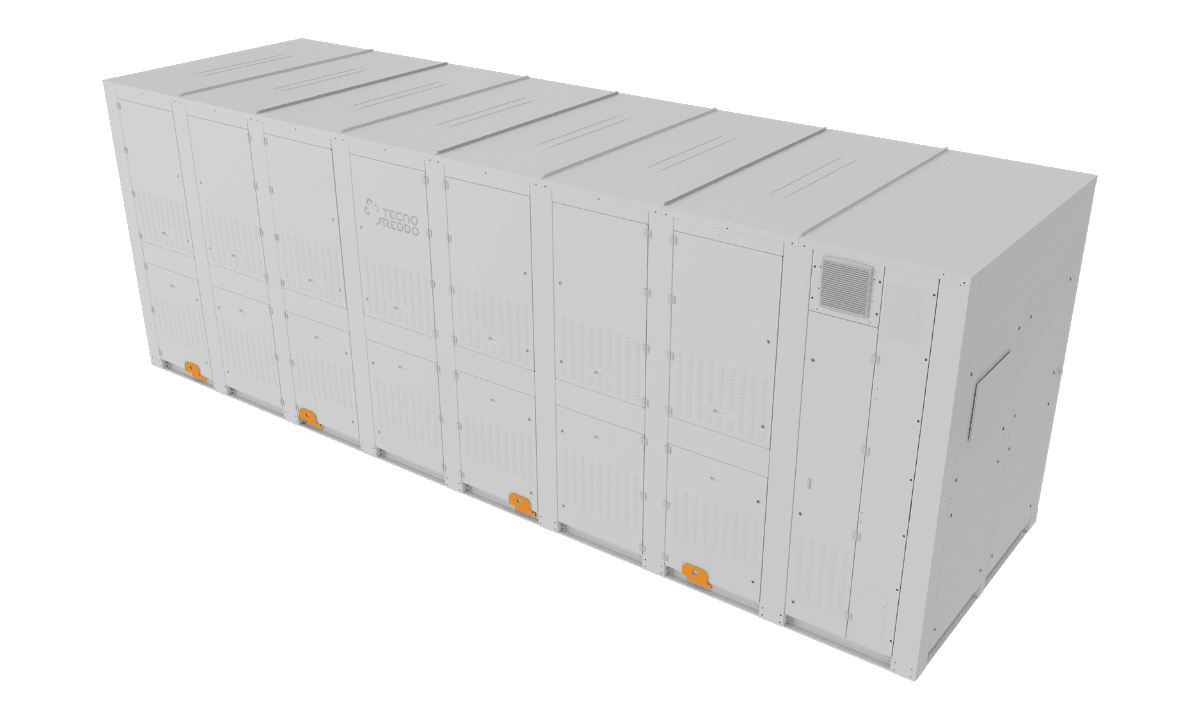
In its Essex factory, English jam producer Wilkin & Sons has replaced four HFC-based low-temperature (LT) 30kW (8.5TR) screw packs with two 60kW (17.1TR) CO2 booster packs produced by Italian manufacturer SCM Frigo.
The company, best known for its Tiptree range of fruit preserves, has produced jam and marmalades since 1885. SCM Frigo is part of the Beijer Ref group. FridgeHUB, operated by Beijer Ref UK & Ireland, designed the CO2 system, supplied the equipment and provided training to the local contractor, Adcock Refrigeration and Air Conditioning.
“We firmly believe that this project represents a model for successful refrigeration system upgrades,” said Michal Wiecaszek, Head of FridgeHUB, in the ACR Journal. “The innovative approach to design, technology selection, and collaborative support sets a new benchmark within the industry.’’
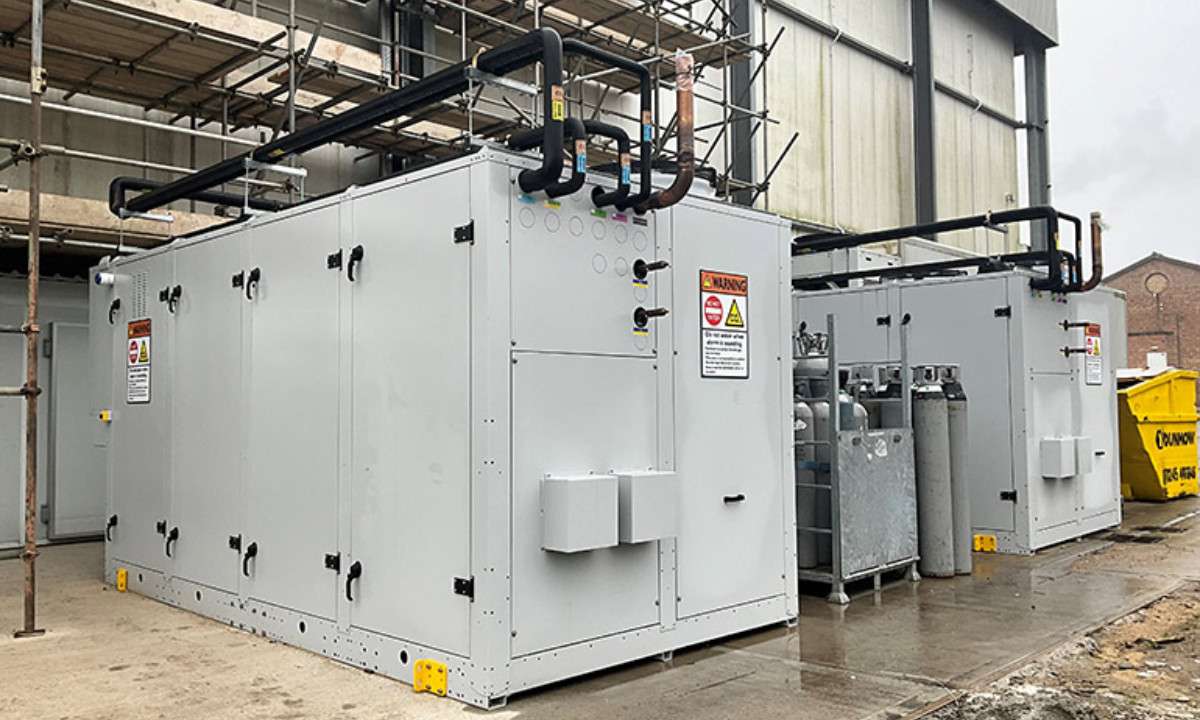
The project: The aged HFC equipment, set at the jam makers required −31°C (−23.8°F) SST, persistently leaked. A glycol-based system temporarily solved the jam maker’s freezer reliability issues.
- The limited installation space and the large LT load ultimately led the designers to a CO2 solution installed outdoors, which will also support the high-temperature (HT) tempering facility planned in the second phase of the project. Ammonia (R717), HFO and A2L systems, though considered, were rejected for various reasons, including initial cost, operating cost, sustainability and flammability, according to the ACR Journal.
- Two Güntner 30kW evaporators support each of the SCM Frigo 60kW CO2 booster packs.
- Each SCM Frigo unit supplies 28‒100% of the required cooling capacity, allowing the site to manage future LT loads.
Multiple use: The initial efficiency estimate of the CO2 system is 5% higher than that of a traditional synthetic system. However, the design integrated a glycol plate heat exchanger for future tempering rooms, which supports long-term efficiency gains.
- An onboard gas cooler in the CO2 pack rejects heat with the LT compressors feeding the HT compressors and inverters on the lead compressor of both temperature sets.
- Based on the stage of jam making, tempering rooms require temperatures ranging from 35 to 85°C (95 to 185°F).
Learning the ropes: In its first CO2 project, Adcock installed Wilkin & Sons’ new refrigeration system with help from the Beijer Ref UK and Ireland teams.
- Adcock engineers participated in CO2 training at the Beijer Ref Academy in Wetherby, England.
- “The FridgeHUB team gave us the confidence to proceed with the project and the technical support from SCM in the UK provided crucial back-up,” said Paul Parfitt, Director at Adcock.
Other SCM Frigo news: The manufacturer continues to invest in large-scale CO2 equipment with two recent installations: one in France and one in Ecuador.
- The company delivered a 1.5 MW (426.5TR) plug-and-play CO2 transcritical rack system providing 6°C (42.8°F) cooling to a cosmetics and pharmaceutical company. The system includes 1MW (284TR) of heat recovery for space heating and hot water production.
- An integrated 6MW (1,700TR) transcritical CO2 (R744) refrigeration system in a shrimp-processing warehouse supplies temperatures for multiple applications. These include freezing at −45/−42°C (−49/−44°F), LT at −32/−25°C (−26/−13°F), medium temperature at −5/−3°C (23/27°F), a 1°C (34°F) glycol brine and facility HVAC heating and cooling.
“This project represents a model for successful refrigeration system upgrades.”
Michal Wiecaszek, Head of FridgeHUB